Two cartridges can carry the same 5 µm label, fit the same 30-inch housing, arrive in nearly identical cartons, and still behave like completely different pieces of equipment once viscosity rises, solids loading jumps, or the differential-pressure curve starts climbing during a real production run.
Then it fails.
Maybe the pleat pack folds over. Maybe the media blinds before the shift ends. Or—this one’s nastier—the seals bypass while the pressure gauge keeps showing a perfectly respectable number.
Same micron rating. Totally different outcome.
That’s why I don’t trust a cartridge specification that begins and ends with “5 micron, PP material, 20-inch length.” It’s not enough. Not even close.
The right industrial filter cartridge has to remove the target contaminant at the actual operating flow, viscosity, temperature, pressure, and chemical exposure. It also needs to do that without starving the pump, crushing the core, shedding fibres, rolling an O-ring out of its seat, or turning every cartridge change into a two-hour shutdown.
Yet buyers still ask the same question:
“What’s your cheapest 5-micron filter?”
I understand why. Micron ratings are easy to compare. Pressure-drop curves, beta ratios, seal chemistry, contaminant morphology, dirt-holding capacity, and loaded-flow behaviour take more work.
But here’s the ugly truth: buying on micron rating alone isn’t technical procurement. It’s specification theatre.
“Dirty water.”
That description appears in RFQs more often than it should, and frankly, it tells us almost nothing.
What’s making the water dirty? Silica grit? Pipe scale? Fe₂O₃ rust? Activated-carbon fines? Polymer fluff? Algae? Cutting oil? Weld slag? Soft biological sludge?
Different dirt. Different fight.
A hard, angular 20 µm mineral particle may hit the upstream face and stay there. A soft 20 µm biological agglomerate can deform, smear across the media, bridge several openings, or squeeze into a pore network that would easily stop a rigid test bead.
Soft solids cheat.
Sticky gels are worse. They don’t just fill pores; they mud the surface, glue neighbouring particles together, and build a low-permeability cake that sends delta-P upward far faster than a clean laboratory challenge would suggest.
And dissolved contamination? That’s another job entirely.
A normal particle cartridge doesn’t remove a dissolved chemical simply because the molecule is smaller than the filter’s pore rating. Depending on the target, the treatment train may need activated carbon, ion exchange, oxidation, precipitation, nanofiltration, reverse osmosis, or several stages working together.
PFAS is a useful reality check. EPA’s April 2024 rule established enforceable drinking-water limits of 4.0 parts per trillion for PFOA and PFOS, plus 10 ppt limits for PFHxS, PFNA, and HFPO-DA. In May 2026, EPA proposed retaining the PFOA and PFOS limits while rescinding the other three individual limits and the associated Hazard Index regulation; those 2026 changes remain proposals, not final replacements for the 2024 rule. EPA’s PFAS drinking-water regulation makes one point painfully clear: an ordinary sediment cartridge isn’t automatically a dissolved-PFAS treatment device. (US EPA)
So, before discussing cartridge material, collect the dirty details:
“Brown particles” still doesn’t count.
I frankly believe a rough microscope image and a basic gravimetric solids test are often worth more than twenty glossy filter brochures. At least the dirt can’t use marketing language.
A filter cartridge micron rating gives a particle-size reference.
That’s all.
It doesn’t automatically tell you the removal efficiency, dirt capacity, test fluid, flow rate, loading condition, or terminal differential pressure. And without those details, the number can be surprisingly slippery.
A nominal rating usually means the cartridge removes some proportion of particles around the stated size.
How much?
Good question.
A nominal 10 µm cartridge might remove 60% of particles around 10 µm. Another might remove 90%. Both may still be sold as “10 micron,” even though their downstream particle counts look nothing alike.
The result depends on things such as:
If the supplier won’t state the efficiency percentage and test method, you don’t have a complete filtration specification.
You have a sticker.
An absolute rating should connect a stated particle size to a defined removal efficiency under documented test conditions.
Should.
The word “absolute” gets stretched in some catalogs, so I’d still ask for the actual efficiency curve. A bold adjective isn’t test data.
One useful measurement is the beta ratio:
[ \beta_x = \frac{\text{number of upstream particles larger than }x} {\text{number of downstream particles larger than }x} ]
The corresponding efficiency is:
[ \text{Efficiency} = \left(1-\frac{1}{\beta_x}\right)\times100 ]
| Beta ratio | Corresponding efficiency |
|---|---|
| β₂ | 50% |
| β₂₀ | 95% |
| β₇₅ | 98.67% |
| β₂₀₀ | 99.5% |
| β₁₀₀₀ | 99.9% |
For hydraulic filtration, ISO 16889:2022 defines a multi-pass test with continuous contaminant injection. It covers particulate removal, contaminant capacity, and differential-pressure characteristics under stated challenge conditions. It isn’t the correct universal protocol for every industrial gas or liquid cartridge—but it shows what useful performance data looks like. (ISO)
Compare these:
10 µm high-efficiency industrial filter
10 µm(c), β₁₀ ≥ 200, tested under stated ISO 16889 conditions
One sounds reassuring.
The other is measurable.
That gap matters when the downstream component is a servo valve, spray nozzle, membrane skid, chromatography system, dosing pump, bearing, heat exchanger, or finished product.

Where should the captured dirt end up?
That question sounds basic. It isn’t.
Surface filtration catches most particles close to the upstream face of the media. Pleated membranes, screens, wire mesh, and similar structures rely heavily on this mechanism. They can deliver sharp retention and, when the filter cake releases cleanly, reasonable washability.
Depth filtration distributes contamination through a thicker porous path. Melt-blown PP, fibrous media, graded-density cartridges, and certain sintered structures hold particles inside the media body rather than stacking everything on the outer skin.
Neither design wins every time.
A pleated element may have impressive square metres of media tucked inside a compact shell, but sticky process sludge can bridge the pleats, glue the valleys shut, and wipe out that theoretical area much faster than the catalog suggests.
Big area. Tiny benefit.
A depth filter may swallow more dirt before reaching the terminal delta-P. But once particles are buried deep in the matrix, cleaning them out can be frustrating—or impossible.
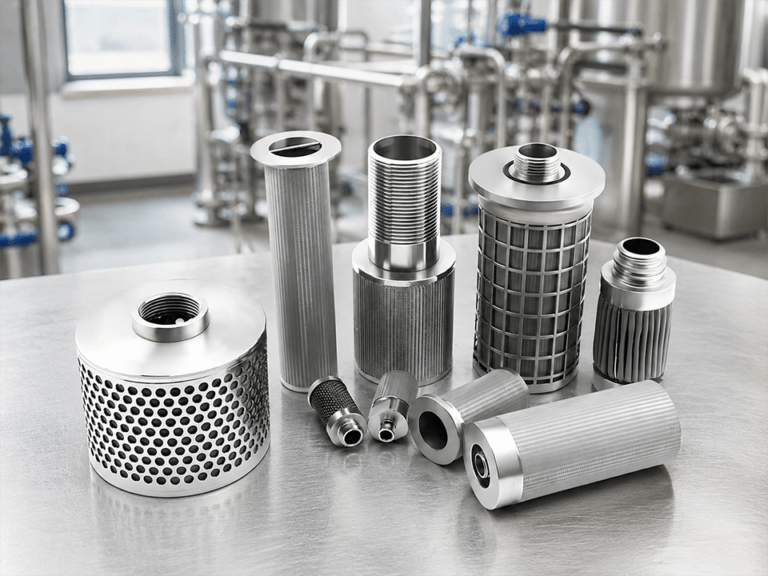
For routine suspended solids, cooling water, general prefiltration, and relatively low-cost disposable service, compare industrial sediment filter cartridges, including melt-blown, pleated, high-flow, and PP configurations.
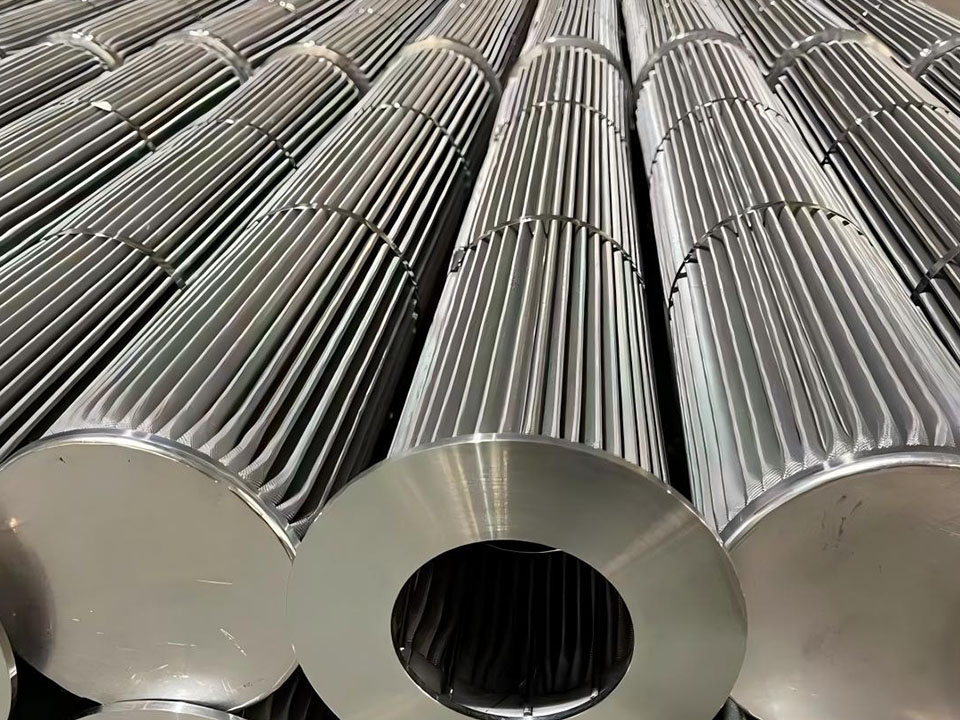
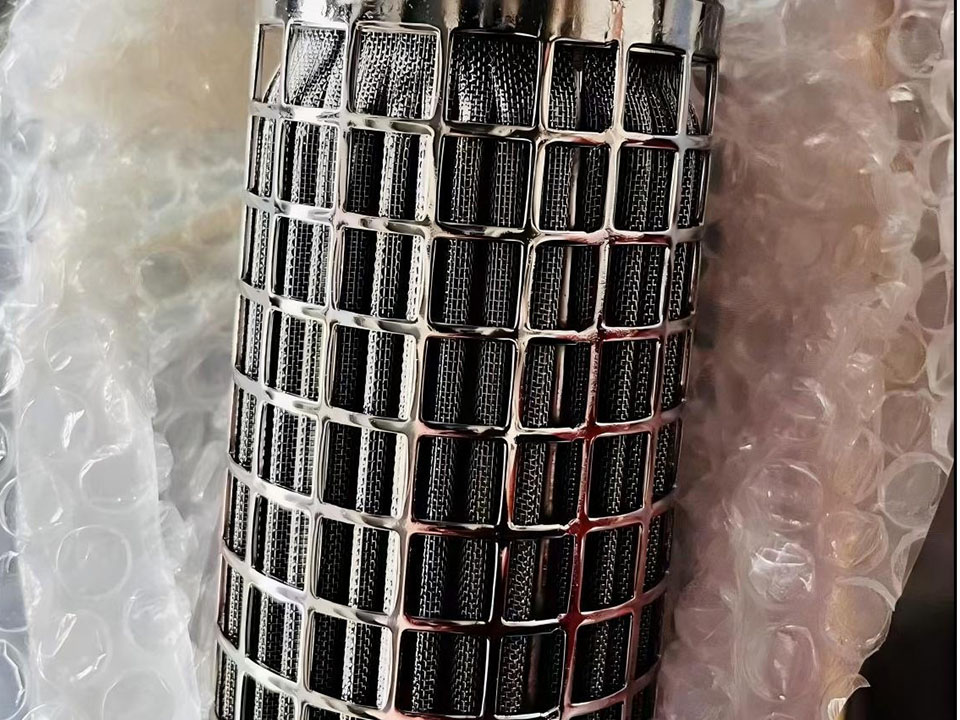
For rigid porous structures, unusual shapes, low-shedding media, controlled gas diffusion, or mechanically supported designs, sintered plastic filter cartridges may be considered in PE, PP, PTFE, nylon, and other engineering plastics.
But don’t select between them from a product photo.
A white cylinder tells you very little.
“PP is compatible.”
Maybe the media is.
What about the core, cage, end cap, thermal weld, adhesive, potting compound, support rod, spring, adapter, gasket, and O-ring?
A filter cartridge is an assembly—not a loose piece of media floating inside a housing. One chemically weak component can ruin the whole build, even when the main filter material looks pristine after exposure.
I’ve got a strong opinion on this: compatibility charts are used far too casually.
A chart may show polypropylene as resistant to sodium hydroxide. Fine. But was that 2% NaOH at 20°C, or 30% NaOH at 80°C with pressure cycling and a weekly hot-CIP sequence?
Those aren’t the same duty.
Not remotely.
Material resistance changes with concentration, temperature, exposure duration, mechanical stress, and chemical mixtures.
That last one gets missed.
A polymer may tolerate Chemical A and Chemical B separately, then soften or stress-crack in the actual mixed process stream. Add elevated temperature—and suddenly the “compatible” cartridge starts swelling around the end cap.
Your review should include:
“Dilute acid” is not enough.
HCl, HNO₃, CH₃COOH, H₂SO₄, and HF don’t behave alike merely because somebody placed them in the same spreadsheet column.
PP and PE are common candidates for water, many acids and alkalis, and general process-liquid service. But actual limits depend on polymer grade, temperature, oxidation, solvent exposure, mechanical load, and construction method.
PTFE provides broad chemical resistance and useful hydrophobic behaviour. Still, it’s not magic. Support geometry, wettability, sealing, permeability, creep, and cost remain part of the decision.
Nylon or PA can offer good wear resistance and mechanical strength. Moisture absorption, dimensional movement, strong acids, and certain solvents need closer review.
304 and 316L stainless steel bring heat tolerance, weldability, cleanability, and mechanical support. Yet “stainless” doesn’t mean “nothing can touch it.” Chlorides, crevices, reducing acids, and high temperature have wrecked plenty of overconfident designs.
Titanium can make sense where corrosion resistance, temperature, and service life justify the higher material and fabrication cost.
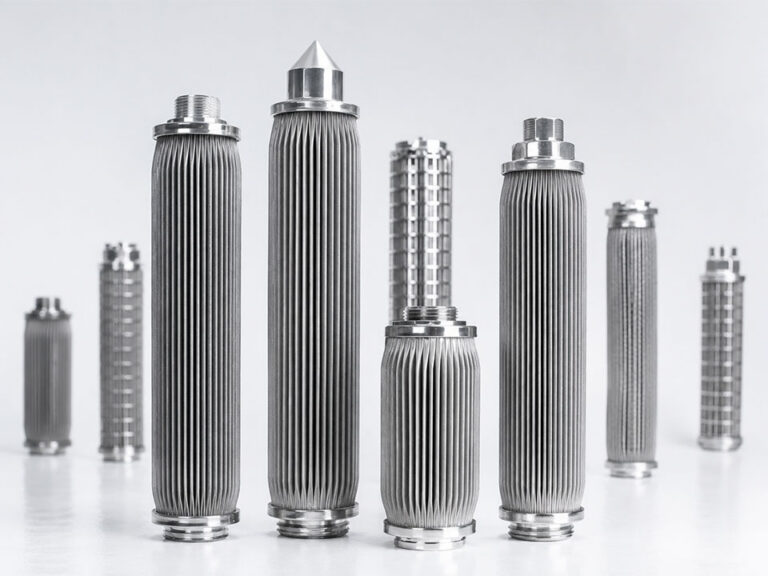
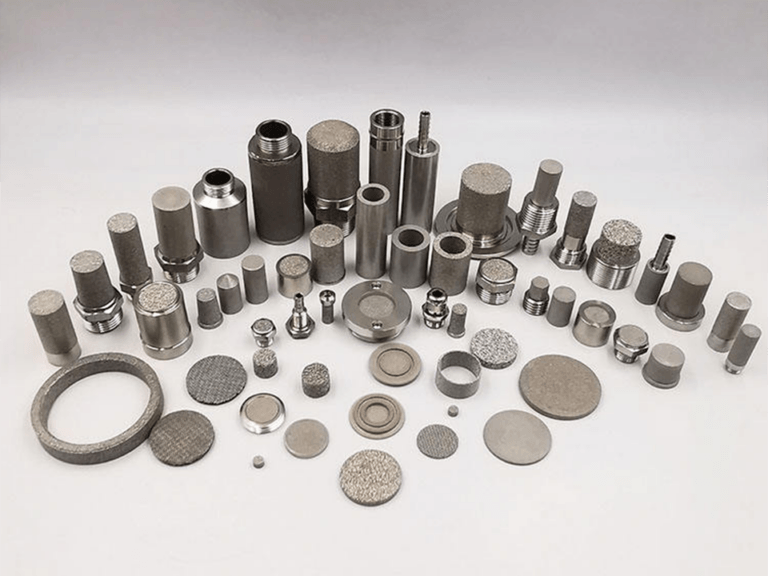
For catalyst recovery, hot gas, high-pressure liquid, repeated backflushing, corrosive process duty, or harsh cleaning cycles, examine available sintered metal filter cartridge structures.
And when a supplier says “chemical resistant,” ask the annoying follow-up.
Resistant to what?
The media can be perfect and the filtration result can still be terrible.
How?
Bypass.
A damaged, undersized, swollen, twisted, or chemically softened seal lets dirty fluid travel around the cartridge rather than through it. The pump keeps running. Flow looks healthy. Delta-P may stay low.
Everyone feels relaxed.
Meanwhile, unfiltered product is heading downstream.
That’s why DOE ends, flat gaskets, 222 O-rings, 226 O-rings, bayonet adapters, threaded ends, flanges, springs, and custom seats shouldn’t be treated as minor connection details.
Check:
EPDM, FKM, silicone, NBR, and PTFE-encapsulated seals all have different strengths and weak points around steam, hydrocarbons, oxidizers, acids, bases, and solvents.
The O-ring is cheap.
The bypass isn’t.

“What’s the flow rate?”
I don’t like answering that without more information.
Flow of what? At what temperature? Through which cartridge length? At what clean differential pressure? Using inside-out or outside-in flow? And how much pressure head does the process actually have available?
A filter cartridge flow rate isn’t a fixed number burned into the end cap.
It changes with:
For laminar flow through porous media, Darcy’s law provides a useful approximation:
[ \Delta P = \frac{\mu L v}{k} ]
Where:
In plain language: when viscosity increases, pressure drop generally increases too—assuming the other conditions remain reasonably similar.
This isn’t exotic theory.
Yet room-temperature clean-water data still gets pasted into specifications for cold gear oil, resin, syrup, coating slurry, polymer dope, concentrated cleaning solution, and fluids that don’t behave remotely like water.
Then the skid starves.
One maximum-flow number isn’t enough.
Ask for pressure drop versus flow, along with:
And compare equivalent data.
A compressed-air curve, clean-water curve, and ISO VG 32 oil curve aren’t interchangeable just because the horizontal axis says “flow.”
Pressure loss isn’t merely a gauge problem. In compressed-air systems, operators often compensate for dirty filters by raising discharge pressure—which feels like a quick fix but turns cartridge restriction into an ongoing electricity bill.
According to the U.S. Department of Energy’s compressed-air sourcebook, a 2 psi increase in discharge pressure around a 100 psig system raises energy consumption by approximately 1% at full output. When 30%–50% of demand is unregulated, the combined penalty may reach about 1.6%–2% for every additional 2 psi. (The Department of Energy’s Energy.gov)
That number doesn’t sound dramatic.
Until the compressor runs 8,000 hours a year.
The same DOE guidance recommends checking pressure differentials across treatment equipment—including filters—and comparing them with manufacturer limits because high pressure loss signals that service is required.
An undersized or overloaded cartridge therefore causes two bills: replacement cost and energy cost.
Nice little trap.
Average flow makes the spreadsheet look calm.
Peak flow finds the weak point.
Cartridge filter sizing should start with the maximum credible process demand—not the comfortable arithmetic mean taken from last month’s operating report.
A simplified area relationship is:
[ A = \frac{Q}{J} ]
Where:
For multiple cartridges:
[ N = \frac{Q{\text{design}}}{Q{\text{approved per cartridge}}} ]
Then add margin.
How much margin? That depends on contaminant variation, viscosity swings, batch peaks, startup crud, expected fouling rate, redundancy requirements, and future production plans.
Not a fashionable answer, I know.
But “always add 10%” is lazy engineering.
Assume the process requires 60 m³/h.
Testing with the actual liquid indicates that one 40-inch cartridge can handle 10 m³/h at the selected clean differential pressure.
The theoretical count is:
[ 60 \div 10 = 6\text{ cartridges} ]
Add a 25% operating margin:
[ 6 \times 1.25 = 7.5 ]
That normally means selecting at least eight cartridges, subject to housing arrangement, loaded pressure drop, solids capacity, batch duration, and standby requirements.
But here’s the snag.
Was the 10 m³/h rating measured with the real process fluid, or with clean water at 20°C? If the production liquid is five times more viscous—or thickens during a cold startup—the six-cartridge base calculation may already be nonsense.
Use real viscosity.
Better yet, run a pilot.
A low purchase price can hide a very expensive cartridge.
Procurement sees $40 per element. Operations sees ten change-outs, ten depressurization cycles, ten chances to pinch a seal, ten housing cleanups, ten disposal events, and several hours of production that never reaches the customer.
Different maths.
A practical annual-cost calculation is:
[ \text{Annual filtration cost} = \text{cartridges} + \text{labour} + \text{downtime} + \text{energy} + \text{cleaning} + \text{disposal} + \text{quality losses} ]
Suppose Cartridge A costs $40 and lasts three days.
Cartridge B costs $160 and lasts thirty days.
The spreadsheet buyer sees a 300% price premium. The plant sees roughly ten cartridge interventions versus one, along with flushing, product heel, labour, waste handling, restart instability, and the possibility of an installation mistake.
Which one costs more?
Exactly.
That’s why reusable sintered metal filter cartridges can make financial sense in severe, washable service, while lower-cost sediment cartridges remain sensible for disposable prefiltration.
But reusable doesn’t automatically mean economical.
A cartridge that needs four hours, three chemical baths, ultrasonic cleaning, hot rinse water, and a full inspection to recover only 60% of its original permeability isn’t necessarily saving money.
It may just be expensive twice.

A regulatory concentration limit tells you the outcome that must be controlled.
It doesn’t select the cartridge.
In February 2024, EPA strengthened the primary annual PM2.5 ambient-air standard from 12.0 µg/m³ to 9.0 µg/m³. EPA’s 2024 particulate-matter decision doesn’t prescribe a particular industrial dust cartridge, but it does underline a basic filtration fact: you can’t judge fine-particle control by looking at an exhaust plume. (US EPA)
For air and gas filtration, distinguish among:
Coarse grinding dust isn’t oil mist.
And smoke isn’t sand.
A cartridge that handles one challenge nicely may be useless against another, even when both streams appear “dusty” to the naked eye.
Looks clean?
Measure it.
In sterile processing, cartridge selection is only the opening move.
The filter must be installed, wetted, sterilized, tested, reviewed, and documented correctly. A qualified membrane inside a badly controlled process is still a badly controlled process.
Sometimes the media isn’t the main problem.
The records are.
A February 2025 FDA warning letter described production filter-integrity testing conducted in July and August 2024. One group of four post-use tests included three failures followed by a passing result; another group of nine tests included five failures, three aborted tests, and a final passing result. FDA stated that operators reported only the passing results. The FDA enforcement record is an uncomfortable reminder that a pass printed after repeated failures doesn’t erase the earlier data. (U.S. Food and Drug Administration)
For validated service, define:
I’d be suspicious of any high-risk filter proposal built around three phrases:
“0.2 micron.”
“Pharmaceutical grade.”
“Widely used.”
Grade isn’t evidence.
And popularity isn’t validation.
| Process condition | Suitable starting point | Main selection data | Common purchasing mistake |
|---|---|---|---|
| General water prefiltration | Melt-blown PP or pleated sediment cartridge | Solids load, particle distribution, flow, change-out ΔP | Buying the smallest micron rating available |
| High-flow process water | Large-diameter pleated or high-flow cartridge | Peak flow, effective area, housing capacity, clean and loaded ΔP | Sizing from average flow |
| Aggressive chemicals | PTFE, compatible PP, selected metal or engineered material | Exact chemical, concentration, temperature, seals, cleaning method | Checking media but ignoring end caps and O-rings |
| Hot gas or high-pressure liquid | Sintered stainless steel, titanium, supported metal media | Temperature, operating pressure, differential pressure, cyclic load | Confusing line pressure with cartridge differential-pressure strength |
| Viscous oil, resin, syrup, or polymer | High-area pleated or engineered porous cartridge | Viscosity at operating temperature, solids load, acceptable flux | Using clean-water flow data |
| Abrasive solids | Supported metal, sintered metal, or durable depth media | Particle hardness, concentration, velocity, erosion risk | Selecting fragile media without mechanical support |
| Sticky gels or biological solids | Low-flux depth media or staged filtration | Deformability, biofilm potential, sanitization, surface loading | Expecting easy backwashing without trials |
| Sterile or contamination-sensitive fluid | Validated membrane cartridge and compatible hardware | Retention validation, extractables, integrity testing, sterilization cycles | Treating “0.2 µm” as proof of sterility |
| Compressed air | Particulate, coalescing, and adsorption stages as required | Aerosol size, oil carryover, dew point, pressure drop, air quality class | Installing unnecessary filtration stages that waste pressure |
| Reusable severe-duty service | Sintered plastic or sintered metal cartridge | Cleaning recovery, mechanical strength, pore stability, lifecycle cost | Assuming every reusable cartridge returns to original performance |
Ever received a quotation showing dimensions, material, micron rating, and price—but nothing about retention efficiency, dirt capacity, clean delta-P, collapse strength, or test conditions?
That isn’t a technical proposal.
It’s a checkout page.
The best filter cartridge for industrial use should survive a document review before anybody opens the housing.
Ask the supplier for:
A capable industrial filtration factory should be able to explain how dimensions, pore structure, assembly, raw materials, and finished-element performance are controlled.
Machine photographs are fine.
Data’s better.
When a standard cartridge doesn’t match the housing, connection, cleaning cycle, operating envelope, or required geometry, custom OEM/ODM filter cartridge development can define the material, dimensions, adapter, seal, pore structure, testing, packaging, and acceptance criteria before full production begins.
Before production.
Not after the first batch won’t fit.
First, document the process. Record the fluid or gas, exact composition, temperature, operating viscosity, normal pressure, peak pressure, design flow, batch duration, and cleaning method.
Then inspect the contamination. Use particle counts, microscopy, size-distribution analysis, gravimetric solids, or laboratory identification—whatever the failure risk justifies.
Define the actual result. Protecting a transfer pump isn’t the same as polishing a final pharmaceutical ingredient. State the downstream cleanliness limit, equipment-protection target, or product-quality requirement.
Choose the filtration mechanism. Screening, depth filtration, membrane retention, coalescence, adsorption, and staged filtration solve different problems.
Verify every wetted component. Include media, core, cage, seals, supports, end caps, potting compounds, adhesives, welds, and hardware.
Size from pressure-drop data. Use peak flow and actual operating viscosity. Add a realistic loading margin rather than assuming the cartridge stays clean forever.
Run a controlled trial. Measure clean delta-P, flow, removal efficiency, loading rate, product quality, terminal pressure, service life, and cleaning recovery.
Freeze the approved specification. Don’t let purchasing substitute an “equivalent 10-micron filter” merely because the length, diameter, and printed micron number match.
Same size isn’t same performance.
Not remotely.
The best industrial filter cartridge is the element whose verified retention efficiency, media and seal materials, effective area, clean pressure drop, differential-pressure strength, temperature limit, and maintenance method match the real fluid, contaminant distribution, peak flow, required cleanliness, operating cycle, and cost of failure.
For ordinary sediment prefiltration, a PP depth or pleated cartridge may be the sensible choice. For heat, high delta-P, corrosive fluids, repeated cleaning, or severe mechanical duty, a sintered metal or engineered sintered-plastic element may offer better lifecycle economics.
But there’s no universal winner.
Anyone naming the “best” cartridge without seeing the process data is guessing.
A nominal micron rating indicates that a filter removes a manufacturer-defined proportion of particles near the stated size, whereas an absolute rating should connect that particle size to a documented efficiency or beta ratio under specified test conditions, making absolute performance data more useful for engineering comparisons.
Still, don’t accept “absolute” on faith.
Request the test standard, test contaminant, flow, fluid, viscosity, loading method, terminal pressure drop, and efficiency curve. The fine print isn’t decoration—it’s the performance claim.
Cartridge filter sizing is the process of providing enough effective media area and enough parallel elements to handle peak design flow at actual operating viscosity while keeping clean and loaded differential pressure inside the limits of the cartridge, housing, pump, compressor, seals, and production process.
Start with the validated flow per cartridge. Divide peak process flow by that figure, then add margin for fouling, viscosity movement, batch variation, standby capacity, startup contamination, and future production increases.
And don’t round down.
The process won’t care that seven cartridges were cheaper than eight.
Filter cartridge material compatibility is the confirmed ability of every wetted component—including media, core, cage, end caps, adhesives, O-rings, gaskets, and hardware—to tolerate the actual chemical, concentration, temperature, pressure, exposure time, cleaning agents, sterilization cycles, and credible process upsets without degrading or contaminating the product.
Use a compatibility chart for initial screening.
Then obtain a full material declaration, written supplier confirmation, immersion-test data where appropriate, and evidence from a representative process trial. The component that fails is often the one missing from the original chart.
An industrial filter cartridge should be replaced or cleaned when differential pressure reaches the validated terminal limit, required flow can no longer be maintained, contaminant breakthrough occurs, product quality drifts, integrity testing fails, or an approved time-based service interval expires—whichever condition arrives first.
Time-based replacement may be necessary in validated hygiene processes. In less regulated systems, delta-P and performance trending usually prevent both premature disposal and dangerous overuse.
Don’t wait for collapse.
That’s failure, not maintenance.
Filter cartridge pressure drop is the measurable resistance created as liquid or gas passes through the housing, media, supports, seals, and accumulated contamination; excessive resistance can cut process flow, increase pump or compressor energy, deform the element, open bypass paths, upset production, and shorten service life.
Record the clean differential pressure immediately after installation.
Then trend it against throughput, operating hours, temperature, viscosity, and batch conditions. Otherwise, “it normally lasts two weeks” remains plant folklore instead of useful maintenance data.
An industrial filter cartridge selection shouldn’t begin with a catalog image and end with the lowest price per piece.
Start with the process.
Send the fluid or gas composition, contaminant information, required removal efficiency, design flow, operating viscosity, temperature, normal pressure, maximum differential pressure, cartridge dimensions, connection style, cleaning method, current failure mode, and estimated quantity.
LVYN Filtration can review those details and develop a sintered plastic, sintered metal, sediment, or custom-engineered cartridge around the actual duty.
Not a vague micron number.
The actual duty.